
任务4:射线检测与流程
NOTE: The CMM or SB takes precedence. Otherwise, refer to ASTM E1742 for the radiographic inspection procedure to inspect parts or materials. When and X-ray is required, keep the film for at least 5 years.
注:CMM或SB规范优先适用。否则参照ASTM E1742标准执行零件或材料的射线检测程序。当需使用X射线时,底片须保存至少5年。
(1) General Data
基本要求
(a) Inspection personnel must meet the certification requirements of Military Specification MIL-STD-410. At least one person must be certified to a level III in the Radiographic test method.
检验人员须符合军用规范MIL-STD-410的认证要求。至少一名人员须持有射线检测方法三级认证。
(b) Radiographic examination of parts or material must be done in accordance with a written procedure as outlined in ASTM E1742. The procedure must include the specific information concerning the facility equipment, materials and process to be used in conjunction with a technique card which contains this same specific information necessary to inspect that part. All procedures and technique cards must be signed and approved by the facility level III certified in the radiographic test method.
零件或材料的射线检测须遵循ASTM E1742规定的书面程序。该程序须包含检测设施设备、材料及工艺的具体信息,并配合载有同等必要检测信息的检测技术卡。所有程序及技术卡均须经设施内射线检测方法三级认证人员签字批准。
(c) The radiographic test technique card must contain all the necessary details used for radiographic inspection for each part. The technique card with the representative radiographs of an actual part or a representative sample of a part must be submitted to Hamilton Sundstrand (HS) Nondestructive Test (NDT)/Quality Engineering for approval before acceptance of hardware. The location and orientation of the parts on the radiographs submitted should define and represent the central and outer most position in the cone of radiation that the parts will be located.
射线检测技术卡须包含各零件检测所需的全部必要细节。技术卡须附有实际零件或代表性样本的代表性射线照片,并在硬件验收前提交给HS(HS)无损检测(NDT)/质量工程部门审批。提交的射线照片中零件的位置与方向应明确并代表零件实际安装时在辐射锥体内的中心位置及最外缘位置。
The technique card must contain at least the following:
技术卡至少应包含以下内容:
1 The company name doing the radiographic inspection.
执行射线检测的公司名称。
2 The revision of the radiographic inspection technique.
射线检测技术修订版本号。
3 Part number.
件号
4 Part name.
件名
5 Engineering drawing revision.
工程图纸修订版本号。
6 Material type and specification identification.
材料类型及规格标识。
7 Radiographic test specification.
射线检测规范。
8 Inspection class and grade acceptance criteria.
检验等级与合格标准。
9 Sensitivity level requirements.
灵敏度要求。
10 Density requirements.
密度要求。
11 X-ray machine identification (machine type, brand, focal spot size, max.KVP/MA output and x-ray tube screens or filters).
X射线机参数(机型、品牌、焦斑尺寸、最大KVP/MA输出及X射线屏或气滤片)。
12 Film processor identification (type, brand and temperature.).
显影机标识(型号、品牌及温度)。
13 X-ray film brand used for the technique.
该技术所用X射线胶片品牌。
14 Penetrameter and block material type.
穿透计及基准块材料类型。
15 Printed identification of the individual who prepared the technique and the approved facility radiographic level III along with the date the technique was developed. Also the signature and date of the approved facility radiographic level III.
技术制定者及经批准的三级射线照相机构的印刷标识,含技术制定日期。另需经批准的三级射线照相机构签名及日期。
16 Each exposure view must identify the following. This information is listed on the technique card.
每张曝光视图必须标识以下信息(技术卡上列明):
• View number.
视图编号
• Actual thickness of the penetrameter block or material used to support the penetrameters for the individual exposure.
该次曝光所用穿透仪块或支撑材料的实际厚度
• Identification of the penetrameters used for the exposure.
该次曝光所用穿透仪的型号
• KVP, MA and Time used for the individual exposure.
该次曝光使用的KVP、MA及曝光时间
• Source to film and object to film distance.
源到胶片与物体到胶片的距离
• Tube to film and part to film angle.
管到胶片与零件到胶片的夹角
• Front and back lead screen thicknesses used for the exposure
曝光所用前后铅屏厚度
• Film speeds used for the exposure. When multiple film techniques are employed, list the speeds in the order from front to back they appear in the cassette during the exposure.
曝光所用胶片感光度。采用多层胶片技术时,按曝光过程中胶片盒内从前至后的排列顺序列出感光度。
• Identify the maximum quantity of parts located on the film during the exposure.
标注曝光胶片上零件的最大数量。
• Provide photographs or a sketch defining the positions and locations of the part and penetrameters on the film in relation to the film and to the tube used for each view.
提供照片或示意图,标明各视图中零件与穿透计在胶片上的位置及与胶片、X射线管的相对关系。
(d) Unless otherwise specified in the CMM, each exposure must meet the 2-2T quality level as defined in ASTM E94.
除非CMM另有规定,每次曝光均须达到ASTM E94标准定义的2-2T质量等级。
(e) All parts and radiographs must be marked so as to be mutually identifiable.
所有零件及射线照片必须标记以确保相互可识别。
(f) Film density on both the penetrameter and in the area of interest for that exposure must be between 1.5 and 4.0 H&D for castings and those situations not requiring penetrameters. All other parts, processes, material types and situations must have a film density on the penetrameter and area of interest of 2.0 to 4.0 H&D. The film density (regardless of the part type or material process) in the area-of-interest must not vary more than +30% or -15% from that of its respective penetrameter.
对于铸件及无需穿透计的情况,穿透计区域与曝光关注区域的胶片密度均须在1.5至4.0 H&D之间。其余所有零件、工艺、材料类型及情况,其透射仪区域与关键区域的胶片密度均须在2.0至4.0 H&D之间。关键区域胶片密度(无论零件类型或材料工艺)与对应透射仪区域的偏差不得超过+30%或-15%。
(g) Multiple Film Exposure Techniques – Multiple film exposures made using two or more films of the same or different speeds in the same film holder is permitted. However, multiple film viewing is not allowed. Each film must be viewed independently and must have the penetrameter density/sensitivity and area-of-interest coverage and density within the requirements of this specification.
多片胶片曝光技术 – 允许在同一胶片夹中使用两片或更多相同或不同感光度的胶片进行多重曝光。但禁止多重胶片同时观察。每片胶片必须单独观察,其探伤仪密度/灵敏度、感兴趣区域覆盖范围及密度均须符合本规范要求。
(h) Equipment Calibration Requirements – Penetrameters, wedges and material blocks must be individually identified as to their material type and serialized for traceability. Alloy or material type identity may be verified by one of the following methods:
设备校准要求 – 穿透仪、楔块及材料块须单独标识材质类型并序列化以确保可追溯性。合金或材质类型可通过以下任一方法验证:
• Spectrographic analysis.
光谱分析法
• Radiographic comparison on a spectrographically analyzed item with one of equal thickness.
将光谱分析后的样品与等厚样品进行射线照相比对
• The penetrameters, wedges and blocks must also be dimensionally verified at least annually with the exception of the following:
除下列情况外,测厚仪、楔块及基准块须至少每年进行一次尺寸验证:
• If the penetrameters are completely covered with a sealed coating of a type that can easily be visually identified, then the coated penetrameters must be initially dimensionally verified and must be checked at least annually for damage and wear. If damage or wear is evident or the coating is removed in any way, the penetrameter must undergo a complete dimensional verification.
若测厚仪表面覆盖可直观识别的密封涂层,则涂层测厚仪须进行初始尺寸验证,并至少每年检查涂层损伤与磨损情况。若出现明显损伤、磨损或涂层剥落,则须进行完整尺寸验证。
• All other equipment calibrations and verifications for the x-ray machine, densitometer, densitometer film strip and film viewer must be check in accordance with and meet the requirements of ASTM E1742.
其余所有设备校准与验证(包括X射线机、密度计、密度计胶片条及胶片观片器)均须符合ASTM E1742标准要求。
(i) Unless otherwise specified, all radiographs used for acceptance of hardware must be retained for a period not less than 6 years from the date the radiographs were made.
除非另有规定,所有用于硬件验收的射线照片须自拍摄之日起保存至少6年。
(2) Safety
安全
(a) While most X-ray equipment is designed to minimize the danger of exposure harmful to personnel, it is essential that adequate measures be taken to protect persons who work with or are near x-ray equipment. These measures may include warning signs, labels, and signals, interlocked enclosures, shielding, the use of survey meters, and monitoring devices such as dosimeters and film badges.
尽管多数X射线设备设计旨在最大限度降低人员受有害辐射的风险,仍必须采取充分措施保护操作或靠近X射线设备的人员。这些措施可包括警示标志、标签及信号、联锁防护罩、屏蔽装置、监测仪的使用,以及剂量计和胶片剂量计等监测设备。
(b) Facilities should comply with the American National Standards Institute (ANSI) Z 54.1 safety standard for non-medical X-ray and sealed gamma-ray sources, also designated National Bureau of Standards handbook 93, Part I (U.S. Department of Commerce). This booklet is for sale by the Superintendent of Documents, U.S. Government Printing Office, Washington, D.C. 20402. It may also be ordered from the American National Standards Institute, 1430 Broadway, New York, N.Y. 10018.
设施应符合美国国家标准协会(ANSI) Z 54.1非医疗X射线及密封伽马射线源安全标准,亦称《国家标准局手册93第一部分》(美国商务部)。该手册可向华盛顿特区20402号美国政府印刷局文件主管处购买。亦可向美国国家标准学会订购,地址:纽约州纽约市百老汇1430号,邮编10018。
(c) Rules and regulations pertaining to personnel exposure are contained in the Occupational Safety and Health Administration (OSHA) Standards as published in the Federal Register CFR, Title 29, Chapter XVII, paragraph 1910.96. This publication may also be ordered from the Superintendent of Documents, U.S. Government Printing Office, Washington, D.C. 20402, or from any regional office of the U.S. Department of Labor.
人员辐射防护相关规则与条例载于《联邦法规汇编》第29卷第十七章第1910.96条公布的职业安全与健康管理局(OSHA)标准。本出版物亦可向美国政府印刷局文献管理处(华盛顿特区20402)或美国劳工部任何地区办事处订购。
(d) Compliance must also be observed with all state and/or local public health regulations.
还必须遵守所有州和/或地方公共卫生法规。
任务5:超声波检测
(1) Any facility chosen to do ultrasonic inspections must be approved by Hamilton Sundstrand.
执行超声波检测的机构须经HS公司批准。
NOTE: The CMM or SB takes precedence. Otherwise, refer to MIL-STD-2154 for Ultrasonic Inspection procedures. 注:以CMM或SB为准。若无相关规定,则参照MIL-STD-2154执行超声波检测程序。
任务6:敲击测试
(1) Refer to the CMM.
参照CMM执行。
任务7:渗透检测前的蚀刻检测
NOTE: This procedure gives you steps to etch a machined part before you penetrant-inspect the part.
注:本程序规定了在对零件进行渗透检测前进行蚀刻的步骤。
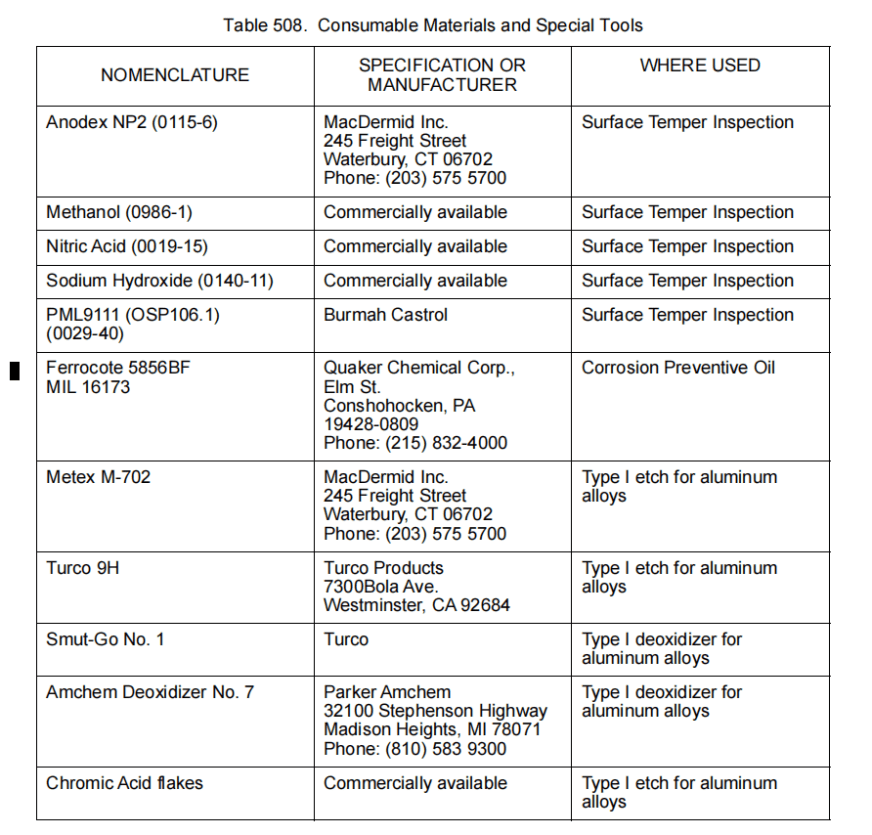
NOTE: Do not etch a part for inspection unless directed to by the CMM. If the CMM orders etching, follow the procedure given there. Refer to the Consumables, Table 508 for etching and desmutting materials.
注:除非CMM指示,否则不得为检测而蚀刻零件。若CMM要求蚀刻,则遵循其中规定的程序。蚀刻及除污材料参见消耗品表508。
任务8:接触式蓝染操作操作指南
(1) General Data
基本数据
(a) Use contact bluing to find incorrect tapers, high spots on surface or similar surface defects.
使用接触式发蓝工艺检测错误锥度、表面凸点及其他类似表面缺陷。
(2) Procedure
操作步骤
(a) Use Dykem Hi-Spot No. 107 as the bluing paste.
发蓝膏选用Dykem Hi-Spot No. 107型号。
(b) Do not mix the bluing paste with water, Vaseline or any other material.
发蓝膏不得与水、凡士林或其他物质混合。
(c) Put some of the bluing paste at regular intervals over the surface of the bluing master.
将蓝化膏以等间距点涂于蓝化基准件表面。
(d) Spread bluing paste in a complete and very thin layer over the surface of the bluing master.
将蓝化膏均匀涂布于蓝化基准件表面,形成完整且极薄的涂层。
(e) Put a blued master in contact with the applicable part surface.
将发蓝基准件与待检零件表面紧密接触。
任务9:低合金钢与普通碳钢零件表面淬火层检测。参照MIL-STD-867标准,验收标准另见HS 972
NOTE: The CMM takes precedence. Otherwise, refer to Military Specification, MIL-STD-867, for surface temper inspection procedure.
注:CMM优先适用。若无CMM,则参照军用标准MIL-STD-867执行表面淬火层检测程序。
NOTE: If you have done a grinding procedure after the final heat treat, you can use this procedure to make sure that the structural properties of the part material have not changed as a result of the grinding.
注:若最终热处理后进行了磨削工序,可采用本程序确保零件材料的结构性能未因磨削而改变。
(1) General Data
基本数据
(a) Do this procedure after the final grind procedure but before you do sand blast, shot peen or other types of surface treatment.
在最终磨削后、喷砂、喷丸或其他表面处理前执行本程序。
(b) Do not do this procedure if the component assembly has parts made of aluminum, brass, bronze, or magnesium or other materials that can be damaged by the solution that will be used.
若部件组装中含有铝、黄铜、青铜、镁或其他易受溶液损伤的材料,不得执行本程序。
(c) Block all blind drill holes to make sure that no acid goes in the drill holes.
封堵所有盲孔,确保酸液不会渗入钻孔。
(d) Make sure you put a protective material over part marks such as electrolytic etch.
必须对电蚀标记等零件标记覆盖保护材料。
(e) Make sure the part surface is clean. Water break surface is required. Refer to Chapter 3, Section 4, Task 1, to alkaline or vapor blast clean the part surface.
确保零件表面清洁,需进行水膜测试。参照第3章第4节任务1,采用碱性或气相喷砂法清洁零件表面。
(f) The effectiveness of the solutions used must be assured by the use of a standard test piece daily before use of etchants in addition to the required solution control system.
除常规溶液控制系统外,必须每日使用标准试样验证蚀刻液效能。
(g) Personnel must be qualified and certified in accordance with MIL-STD-867.
操作人员须符合MIL-STD-867标准资质认证要求。
(2) Procedure
程序
(a) Part must be clean.
零件必须清洁。
(b) Use one of the procedures in MIL-STD-867, or put the part fully into a 2.5 – 3.5% by volume solution of nitric acid in methanol that is at ambient temperature for approximately 20-30 seconds or until desired black film is attained. You can also apply the solution with a brush or swab.
采用MIL-STD-867标准中任一工艺,或将零件完全浸入体积浓度为2.5-3.5%的常温甲醇硝酸溶液中约20-30秒,直至形成所需黑色氧化膜。亦可使用刷子或棉签涂抹溶液。
(c) Flush the part in water at room temperature.
用室温水冲洗零件。
(d) Put the part fully for 30 – 40 seconds into a 3 – 5 oz by weight per gallon solution of sodium hydroxide in water at ambient temperature. You can also apply the solution with a brush or swab.
将零件完全浸入室温下每加仑含3-5盎司(重量)氢氧化钠的水溶液中30-40秒。亦可用刷子或棉签涂抹溶液。
(e) Flush the part in water in room temperature.
用室温水冲洗零件。
(f) Flush the part in hot water that is a minimum of 150 °F (67 °C).
用不低于150°F(67°C)的热水冲洗零件。
WARNING: USE GOGGLES WHEN YOU USE COMPRESSED AIR. MAKE SURE THE AIR PRESSURE IS NOT MORE THAN (30) PSIG. PARTICLES THAT ARE BLOWN BY COMPRESSED AIR CAN CAUSE DAMAGE TO YOUR EYES AND SKIN.
警告:使用压缩空气时必须佩戴护目镜。确保气压不超过30磅/平方英寸(PSIG)。压缩空气吹出的颗粒物可能损伤眼睛和皮肤。
(g) Use a low pressure air gun with clean, dry oil-free air to dry the part.
使用低压气枪,以清洁干燥的无油空气吹干零件。
(h) Optional–Apply a thin layer of Ferrocote 5856BF or equivalent preservative to the surface of the part to be inspected. This aids in inspection.
可选操作——在待检零件表面涂覆薄层Ferrocote 5856BF或等效防腐剂,以辅助检测。
(i) Acceptance Criteria
验收标准
NOTE: A white light intensity of at least 200 foot candles must be available at inspection.
注:检测时需提供不低于200英尺烛光的白光照明强度。
1 Rehardening – Parts that show any evidence of rehardening (untempered martensite) must be subject to rejection.
复硬化——出现任何复硬化迹象(未回火马氏体)的零件必须报废。
2 Abnormal Tempering – Parts that show evidence of abnormal or localized tempering must be evaluated as follows:
异常回火——出现异常或局部回火迹象的零件须按以下标准评估:
a Working Surfaces – Working surfaces of parts such as bearing races, involute sections of gear teeth, areas of tangency of root fillet with involute on gear teeth, cam surfaces, etc. that exhibit abnormal tempering must be subject to rejection.
工作面——轴承圈、齿轮齿渐开线段、齿根圆角与齿轮齿渐开线相切区域、凸轮面等工作面若出现异常回火,必须报废.
b Nonworking Surfaces – Nonworking surfaces of parts such as end faces and top lands of gear teeth, spur and spiral gear root fillets, nonbearing surfaces of bearings, etc. must not exhibit more than 25% of the area abnormally tempered. These abnormally temperated areas must meet the following requirements:
非工作面 – 齿轮齿端面、齿顶、直齿轮与斜齿轮齿根圆角、轴承非承载面等非工作面,异常回火区域面积不得超过25%。此类异常回火区域须满足:
• Abnormal temper indications that break over corners onto working surfaces must be subject to rejection.
异常回火迹象若跨越边角侵入工作面,该零件必须报废.
• Hardness of abnormally tempered areas when measured with a 15 Kg load must not be more than 2 HR15N or 20 VHN points lower than the surrounding adjacent areas. If a hardness test cannot be made due to the location of abnormally tempered areas, the part must be subject to rejection.
异常淬火区域经15千克载荷硬度测试时,其硬度值不得低于周边区域2 HR15N或20 VHN点。若因异常淬火区域位置限制无法进行硬度测试,该零件必须报废。
CAUTION: NO CATHODIC CURRENT IS PERMITTED ON PARTS.
注意:零件表面严禁存在阴极电流。
(j) If oil was used for inspection–Anodically clean the part in a solution of 12 – 18 oz/gal of Anodex NP2. The solution must be at ambient temperature and you will clean the part for 1 to 3 minutes at 4 – 8 volts.
若使用油液检测——需在含12-18盎司/加仑Anodex NP2溶液中进行阳极清洗。溶液须保持环境温度,以4-8伏电压清洗1至3分钟。
(k) Flush the part in water at room temperature.
用室温水冲洗零件。
(l) Flush the part in hot water that is a minimum of 150 °F (67 °C).
用不低于150°F(67°C)的热水冲洗零件。
WARNING: USE GOGGLES WHEN YOU USE COMPRESSED AIR. MAKE SURE THE AIR PRESSURE IS NOT MORE THAN (30) PSIG. PARTICLES THAT ARE BLOWN BY COMPRESSED AIR CAN CAUSE DAMAGE TO YOUR EYES AND SKIN.
警告:使用压缩空气时必须佩戴护目镜。确保气压不超过30磅/平方英寸(PSIG)。压缩空气吹出的颗粒物可能损伤眼睛和皮肤。
(m) Use a low pressure air gun with clean, dry oil-free air to dry the part.
使用低压气枪,以洁净干燥的无油空气吹干零件。
(n) If oil was not used for inspection–Apply a thin layer of Ferrocote 5856BF or equivalent preservative to the surface of the part to be inspected.
若未使用油剂进行检测——在待检零件表面涂覆薄层Ferrocote 5856BF或同等防腐剂。
(o) Inspection Information:
检测要求:
NOTE: A white light intensity of at least 200 foot candles must be available at inspection.
注:检测区域需提供不低于200英尺烛光的白光照度。
1 Reharden: If the part has a light gray to white area that is surrounded by a light brown to black border, do not accept the part.
重新淬火: 若零件出现浅灰色至白色区域,且周围有浅棕色至黑色边界,则该零件不合格。
2 Not Normal Temper on a Very Important Surface. If the part has not normal temper (darker than the adjacent surfaces) on a very important surface such as bearing races, involute section of gear teeth, and cam surfaces, do not accept the part if hardness in that area is 20 HV300 sorter that the adjacent surfaces.
关键表面淬火异常。若关键表面(如轴承圈、齿轮渐开线段、凸轮面)出现淬火异常(比邻近表面暗色),且该区域硬度低于邻近表面20 HV300,则该零件不合格。
3 Not Normal Temper on a Not Important Surface. A not important surface can be the end face and top lands of gear teeth, non-bearing surfaces of bearings. If the not important surface has more than 25% of not normal temper, do not accept the part. If the part has less than 25% of not normal temper, the temper can not go into very important surfaces. Also, the hardness of the not normal temper, when measured with a 33.0 lb. (15 kg) load, must not be less than 2 HR15N points than the area around the not normal temper.
非重要表面出现异常回火。非重要表面包括齿轮齿的端面与顶部台阶、轴承非承载面。若非重要表面异常回火区域超过25%面积,则该零件不合格。若异常回火区域小于25%,则该异常回火区域不得延伸至重要表面. 此外,当采用33.0磅(15千克)载荷测量时,异常淬火区域的硬度不得低于周边区域2 HR15N点。
4 If there is sufficient material for repair of the part in the given limits, then remove the rehardened area or the not normal temper. After the repair is done, repeat the surface temper inspection.
若零件在规定范围内留有足够修复材料,则需清除再硬化区域或异常淬火层。修复后须重新进行表面淬火检测。
任务10:CRES材料的硝酸盐蚀刻
NOTE: The purpose of this procedure is to check for the presence of nitride. This test is applicable only to worn parts. The surface will be steel gray or white before starting.
注:本程序旨在检测氮化物存在。该测试仅适用于磨损零件。起始时表面应呈钢灰色或白色。
(1) General
概述
(a) Use this procedure to determine the presence of Nitride.
采用本程序判定氮化物是否存在。
(b) Protective material must be placed over marks such as electrolytic etch.
电解蚀刻等标记处必须覆盖保护材料。
(c) Part surface must be clean. Water break surface is required. Refer to Chapter 2 to alkaline clean the part surface.
零件表面须清洁,需达到水滴表面。参照第2章进行碱性清洁。
(d) Parts rust easily following etch. Protect parts immediately after etch with Ferrocote 5856BF or equivalent preservative.
蚀刻后零件易生锈,须立即使用Ferrocote 5856BF或同等防腐剂保护。
(2) Procedure
程序
(a) Part must be clean.
零件必须清洁。
(b) Part must be at room temperature.
零件须处于室温状态。
(c) Immerse or swab parts in a 2.5-3.5 volume % nitric acid in methanol at ambient temperature for 20-30 seconds. Time may be extended to 60 seconds to achieve proper discoloration.
将零件浸入或擦拭于室温下2.5-3.5体积百分比的硝酸甲醇溶液中20-30秒。为达到理想变色效果,时间可延长至60秒。
NOTE: Water rinse must begin within 30 seconds of removal from etchant.
注:从蚀刻液中取出后必须在30秒内开始水洗。
(d) Etch by one of the following methods:
采用以下任一方法进行蚀刻:
1 Immerse or swab parts for 5-30 seconds in a solution of 1.5-3.5 volume percent nitric acid (42 degree Baume) in methanol. For immersion applications, water rinsing must begin within 30 seconds of removal of parts from the etchant. For swab applications, water rinsing must begin within 60 seconds from the point at which the material begins to etch.
将零件浸入或擦拭于体积百分比为1.5-3.5%的硝酸(42度波美)甲醇溶液中5-30秒。浸渍操作须在取出零件后30秒内开始水洗;擦拭操作须在材料开始蚀刻后60秒内开始水洗。
2 Immerse or swab parts for 5-45 seconds in an aqueous solution 10 + 2 weight percent ammonium persulfate (NH4)2 S208. For immersion applications, water rinsing must begin within 15 seconds of removal of parts from the etchant. For swab applications, water rinsing must begin within 30 seconds from the point at which the material begins to etch.
将零件浸入或擦拭于10±2%(重量百分比)过硫酸铵(NH₄)₂S₂O₈水溶液中5-45秒。浸渍操作中,零件从蚀刻液取出后须在15秒内开始水洗;擦拭操作中,材料开始蚀刻后须在30秒内开始水洗。
3 Immerse or swab parts for 2-15 seconds in an aqueous solution of 3-15 volume percent nitric acid (42 degree Baume). For immersion applications, water rinsing must begin within 15 seconds of removal of parts from the etchant. For swab applications, water rinsing must begin within 15 seconds from the point at which the material begins to etch.
将零件浸入或擦拭于体积百分比为3-15%的硝酸水溶液(42度波美)中,持续2-15秒。浸泡操作中,零件从蚀刻液取出后须在15秒内开始水洗;擦拭操作中,材料开始蚀刻后须在15秒内开始水洗。
4 Immerse or swab parts for 1-10 seconds in an aqueous solution of 6-27 volume percent nitric acid (42 degree Baume) with 12-16 oz/gal ammonium bifluoride. For immersion applications, water rinsing must begin within 10 seconds of removal of parts from the etchant. For swab applications, water rinsing must begin within 15 seconds from the point at which the material begins to etch.
将零件浸入或擦拭于含12-16盎司/加仑氟化铵的6-27体积百分比硝酸水溶液(42度波美)中1-10秒。浸渍操作中,零件从蚀刻液取出后须在10秒内开始水洗。擦拭应用时,必须在材料开始蚀刻后15秒内开始用水冲洗。
(e) Rinse part in water at room temperature.
用室温水冲洗零件。
(f) Immerse or swab parts in neutralizing solution of 3-5 oz/gallon sodium hydroxide for 30-40 seconds.
将零件浸入或擦拭于3-5盎司/加仑氢氧化钠的中和溶液中,持续30-40秒。
(g) Rinse part in water at room temperature.
用室温水冲洗零件。
(h) Rinse part in hot water (150°F minimum).
用热水(最低150°F)冲洗零件。
(i) Check wet part using pH indication strips. The pH must be in range of 6.4 to 8.3.
使用pH指示试纸检测湿零件。pH值必须在6.4至8.3范围内。
1 If part test result is above 8.3 pH, the part must be rinsed and retested.
若零件测试结果pH值高于8.3,必须冲洗后重新测试。
2 If part test result is below 6.4 pH, the part must be processed through the neutralizing solution (repeat paragraphs (e)-(h) above) and retested.
若测试结果低于pH 6.4,必须经中和溶液处理(重复上述(e)-(h)步骤)后复检。
NOTE: If parts are not to be inspected immediately, apply Ferrocote 5856BF or equivalent to preserve them.
注:若零件暂不检验,须涂覆Ferrocote 5856BF或同等保护剂。
(3) Inspection Criteria
检验标准
(a) Nitrided surfaces must be darkened to gray or black.
氮化表面必须呈现灰黑色。
(b) Not nitrided surfaces must remain bright.
未氮化表面须保持光亮。
(c) Bright surfaces or bright areas surrounded by darkened areas must be tested for the presence or absence of nitride using a clean, sharp file having a hardness of HRC 58-66, such as:
光亮表面或被暗化区域包围的光亮区域,须使用硬度为HRC 58-66的洁净锐利锉刀检测氮化层存在与否,例如:
Half Round #0
半圆锉 #0
Half Round Cut #2
半圆切削锉 #2
Needle Round Cut #2
针状圆切锉 #2
Needle Three Square Cut #2
针状三方切锉 #2
Riffler Style 8 Cut #2
锯齿状8号切锉 #2
Die Sinker Cut #2
沉孔锉 #2
NOTE: Files used for testing should not be used for any other purpose.
注:检测用锉刀不得用于其他用途。
1 File Check Procedure
锉刀检查程序
NOTE: File check must not be done on corners or edges where nitride may become damaged.
注:严禁在可能损伤氮化层的边角区域进行锉刀检查。
a Perform file check on reference blocks to get feel for nitrided versus not nitrided surfaces.
先在标准基准块上操作锉刀,熟悉氮化层与非氮化层的触感差异。
b Place a clean, sharp file against the surface to be checked. Exert constant, moderate, fingertip pressure downward and slide file over the surface.
将洁净锋利的锉刀置于待检表面,以指尖施加恒定适度向下压力,沿表面滑动锉刀。
c Interpretation – If the file slides easily over the surface being tested, the part may be accepted for the presence of nitride case hardness. If the file teeth grip the surface, the area is not nitrided and the hardware is rejected.
判定标准——若锉刀在测试面顺滑移动,则该零件可判定具有氮化表面硬化层;若锉齿咬入表面,则该区域未氮化,硬件应予报废。
任务11:触觉与视觉表面检测
NOTE: This procedure is used to evaluate visual flaws on metallic surfaces by using a stylus over metallic surfaces perpendicular to the lay of the flaw.
注:本程序通过探针垂直于缺陷走向在金属表面移动,评估金属表面的视觉缺陷。
(1) General
概述
(a) Tactilely discrete flaws are not intentional surface defects such as cracks, checks, inclusions, ridges and scratches, which occur infrequently and are not included in roughness average surface measurement. Tactilely discrete flaws can be felt with the finer or fingernail.
可触觉感知缺陷指非人为造成的表面瑕疵,如裂纹、裂痕、夹杂物、棱脊及划痕,此类缺陷发生频率较低且不计入表面粗糙度平均值测量。此类缺陷可用指尖或指甲触觉感知。
(b) The inspection area must have at least 538 lux of light intensity.
检测区域光照强度需≥538 lux。
(2) Inspection Methods – Stylus
检测方法 – 探针
(a) General
总则
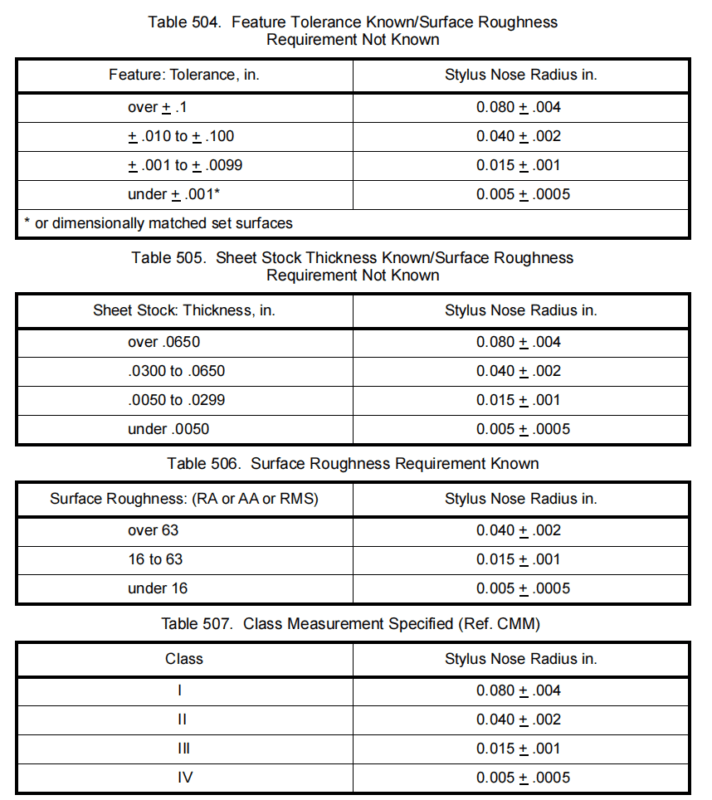
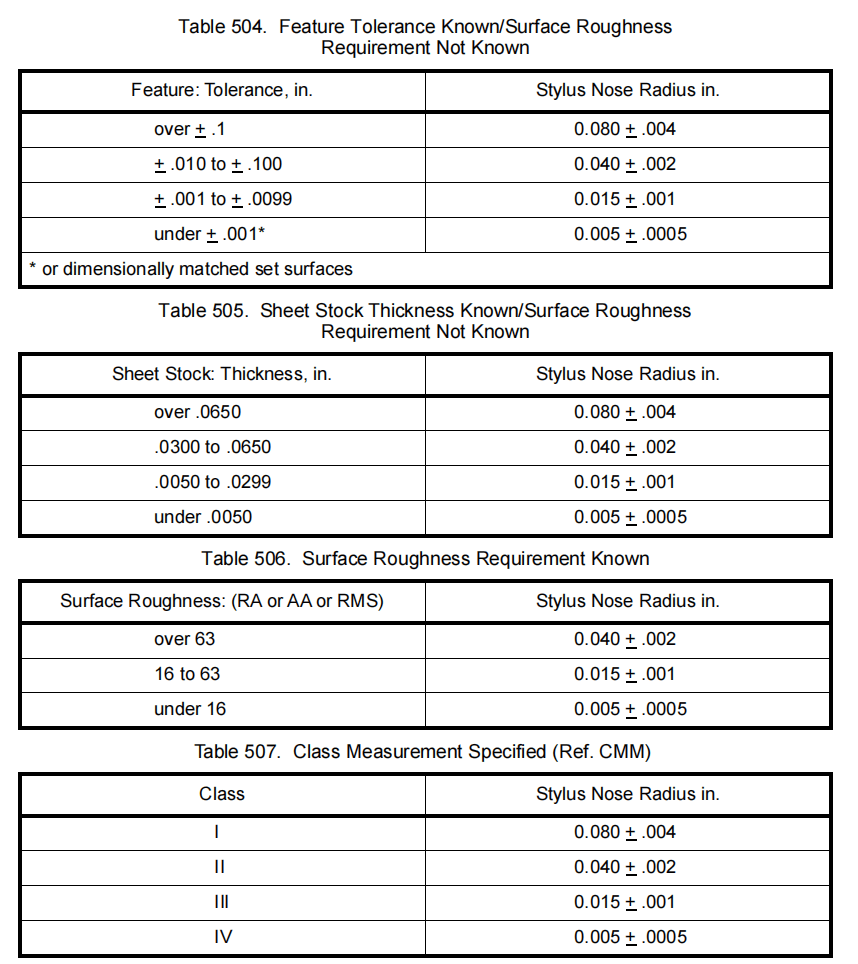
1 Stylus nose radius will vary relative to surface roughness criteria of the finished part. See Table 504, Table 505, Table 506 or Table 507. If the surface roughness requirement is not known, use either feature tolerance or sheet stock thickness as a guide. Refer to Table 504 or Table 505. If surface roughness requirement is known, refer to Table 506. If class of measurement is specified in the Component Maintenance Manual, refer to Table 507.
探针尖端半径需根据成品零件表面粗糙度标准调整。参见表504、表505、表506或表507。若表面粗糙度要求未知,可参照特征公差或板材厚度作为指导,参见表504或表505。若表面粗糙度要求已知,则参照表506。若部件维护手册中规定了测量等级,请参照表507。
2 Inclined Method – Hold stylus between forefinger and thumb at an angle of approximately 60 degrees from horizontal. With stylus tip radius resting lightly on the surface, move tip toward the imperfection.
倾斜法——用食指与拇指握持测针,使其与水平面成约60度角。将测针尖半径轻触表面,朝缺陷方向移动。
3 Perpendicular Method – Hold stylus between forefinger and thumb so that the stylus is perpendicular to the surface. With stylus tip radius resting lightly on the surface, move tip toward the imperfection.
垂直法——用食指与拇指握持测针,使其与表面垂直。使探针尖端半径轻触表面,将尖端移向缺陷处。
4 If the stylus catches momentarily as it is moved across the flaw, the flaw is considered tactilely discrete and is not acceptable.
若探针在移动过程中短暂卡住缺陷,则该缺陷被视为触觉离散缺陷,不可接受。
任务12:硬度测量
(1) General
概述
(a) By definition, the hardness of a metal is the resistance which it exerts against the deformation of its surface.
按定义,金属硬度指其抵抗表面变形的抗力。
(b) The hardness measurement is an indentation measurement using a calibrated machine to force a penetrator into the surface of the material being measured. The dimensions of the remaining imprint provide a measurement of the hardness.
硬度测量采用校准设备实施压痕法,通过压头对被测材料表面施加载荷。残留压痕的尺寸数据即为硬度量值。
(c) Hardness measurements are often used to verify the heat treatment condition of metals or to determine if overtemperature conditions may have occurred during use which change the hardness and strength of the part.
硬度测量常用于验证金属热处理状态,或判定零件使用过程中是否存在过热现象导致硬度与强度变化.
(2) Types of Hardness Measurements
硬度测量类型
NOTE: The CMM defines the type of hardness test required.
注:CMM规定所需硬度测试类型。
(a) Brinell Hardness Measurement per ASTM-E-10
符合ASTM-E-10标准的布氏硬度测量
(b) Vickers Hardness Measurement per ASTM-E-92
符合ASTM-E-92标准的维氏硬度测量
(c) Rockwell Hardness Measurement per ASTM-E-18
符合ASTM-E-18标准的洛氏硬度测量
(d) Portable Rockwell Test
便携式洛氏硬度测试
1 Portable hardness testing equipment is used when the weight, shape, or condition of the part prevents measurement by other methods.
当零件重量、形状或状态不适合其他测量方法时,应使用便携式硬度测试设备。
2 The tester is attached to the surface to be measured or to an adjacent surface.
测试仪应接触待测表面或相邻表面。
NOTE: The portable tester is not considered to be a precise measuring device. It is used only when other testing equipment cannot be practically used.
注:便携式测试仪不属于精密测量设备,仅在其他测试设备无法实际使用时采用。
NOTE: Conversion Tables – no exact method for converting, accurately, from one hardness scale to another exists. Such conversion should be made only when necessary. For standard hardness conversion tables for carbon, low alloy, or magnetic stainless steels, refer to ASTM-E-140.
注:换算表——目前尚无精确转换不同硬度标尺的标准方法。仅在必要时进行转换。碳钢、低合金钢或磁性不锈钢的标准硬度换算表请参阅ASTM-E-140。
任务13:弹簧检验
(1) Procedure 1: Procedure to Inspect Helical Type Springs
方法1:螺旋弹簧检验程序
(a) Identify the type of spring you are to inspect. Two types of springs are:
确定待检弹簧类型。弹簧分为两类:
1 Compression helical springs. This is a coil helical spring that has resistance to a compressive force.
压缩螺旋弹簧。此类螺旋弹簧通过盘绕线圈结构产生抗压缩力。
2 Extension helical springs. This is a closed coil helical spring that has resistance to a force that pulls. The spring has tension in the coils.
伸缩螺旋弹簧。此类闭合盘绕的螺旋弹簧具有抗拉伸力特性,其线圈处于受拉状态。
(b) Find the correct data on the spring you are to inspect.
获取待检弹簧的正确参数。
(c) Find the free length or height of the spring. The free length or height is the maximum length of the spring in a free condition.
确定弹簧的自由长度或高度。自由长度或高度指弹簧处于自由状态时的最大长度。
1 To find the free height of a compression spring, you must put the spring on a reference surface and measure the highest point on the spring.
测定压缩弹簧自由高度时,需将弹簧置于基准面,测量弹簧最高点。
2 To find the free length of an extension spring, you must use a vernier caliper. Measure the free length from the inside surface of the ends of the spring.
测定拉伸弹簧自由长度时,须使用游标卡尺。从弹簧端部内表面起测量自由长度。
(d) Find the load limit. The load limit is the relation between a defined extended length or a compressed height and a given weight or force.
确定载荷极限。载荷极限指规定伸长长度或压缩高度与给定重量或作用力之间的关系。
1 Use an Elasticometer, Link Spring Checker, or Hunter Spring Checker with adapters, or equivalent, to measure the load limit on the spring.
使用弹性计、连杆弹簧检测仪、带适配器的亨特弹簧检测仪或同等设备测量弹簧负载极限。
2 You may have to pre-load the spring before the load limit can be measured. The pre-load will be sufficient value to start to open the end coil.
测量前可能需预加载弹簧,预加载值应足以使端圈开始展开。
(e) If necessary, use one of the steps that follow to find the spring rate:
如需测定弹簧刚度,可采用以下任一方法:
1 The spring rate will be given in the applicable Component Maintenance Manual as two or more specified loads at some specific height.
弹簧刚度值在适用部件维护手册中以特定高度下的两个或多个指定载荷形式给出。
2 The applicable Component Maintenance Manual will tell you to put a load at a specific height and to put one more load at a specific deflection from the initial height.
适用部件维护手册将要求在特定高度施加载荷,并在初始高度的特定偏转量处施加额外载荷。
(2) Procedure 2: Procedure to Inspect Torsion Springs.
方法二:扭力弹簧检查程序。
NOTE: Actual check is very difficult because friction is not predicatable.
注:实际检测难度极高,因摩擦力不可预测。
(a) Use a Hunter Spring Checker to inspect the torsion spring.
使用Hunter弹簧检测仪检查扭力弹簧。
(b) Refer to the applicable Component Maintenance Manual for the correct torsion spring dimensions.
参照适用部件维护手册确认扭力弹簧正确尺寸。
任务14:涂层厚度检测——适用于电镀、喷漆等
NOTE: Direct micrometer readings are always acceptable.
注:直接千分尺读数始终有效。
(1) Procedure 1: Dermitron NDT Thickness Tester or equivalent
方法1:德米特龙无损检测厚度仪或同等设备
NOTE: The Dermitron tester uses the Eddy Current method to measure the coat thickness of a metallic coat on a metallic base. You can also measure a non-conductive coat on a metallic base or a magnetic coat on a non-conductive base.
注:该仪器采用涡流法测量金属基材上金属涂层厚度,亦可测量金属基材上的非导电涂层或非导电基材上的磁性涂层。
NOTE: With any eddy current method, the area being tested must be flat and at least twice the size of the probe.
注:采用任何涡流法时,测试区域必须平整且至少为探头面积的两倍。
(a) Refer to the manufacturer’s manual for data on the operation of the equipment.
设备操作数据请参阅制造商手册。
(b) Put the probe on a bare base metal that is the same as the material to be tested to make sure the zero data point for the standard gage sheet and the base metal is the same.
将探头置于与待测材料相同的裸基底金属上,确保标准量规片与基底金属的零点数据一致。
1 If the base metal data point is larger than the standard gage sheet data point, you must subtract this value from data points on the coated parts. This subtracted value will not be larger than 1/3 of the coat thickness.
若基体金属数据点大于标准测厚片数据点,必须从涂层零件数据点中减去该值。该减值不得超过涂层厚度的1/3。
2 If the base metal data point is less than the standard gage sheet data point, then you must adjust the “Zero” control so that the Thickness readout is zero. Then put the probe on the bare base metal and write the value. You must add this value to the data points on the coated parts. This added value must not be larger than 1/3 of the coat thickness.
若基体金属数据点小于标准测厚片数据点,则需调整“零点”控制旋钮使厚度读数归零。随后将探头置于裸露基材上记录数值。该数值必须加至涂层零件的数据点上,且加值不得超过涂层厚度的1/3。
(c) Put the probe on the part to be measured to get the thickness of the coat.
将探头置于待测零件上获取涂层厚度。
(d) The coat thickness must be in the limits given in the applicable Component Maintenance Manual.
涂层厚度必须符合适用部件维护手册规定的限值。
(e) If the coat thickness is not in the limits given in the Component Maintenance Manual, then you have to remove the coat and apply the coat again.
若涂层厚度超出部件维护手册限定范围,须清除原涂层并重新涂覆。
(2) Procedure 2: Fischerscope NDT Thickness Tester
方法二:Fischerscope无损检测厚度仪
NOTE: The Fischerscope tester can use the Eddy Current or the Magnetic Induction method to measure the coat thickness of conductive or nonconductive coats on conductive and/or magnetic materials.
注:Fischerscope检测仪可采用涡流法或磁感应法,测量导电/磁性基材上导电或非导电涂层的厚度。
(a) Refer to the Manufacturer’s Manual for data on the operation of the equipment.
设备操作数据请参阅制造商手册。
消耗品
NOTE: Maintenance personnel must use the specified consumable material for the specified task. These consumable materials are known to agree with all of the design and qualification requirements. Only approved materials engineering personnel can make equivalent consumable material decisions. These materials are used at the risk of the organization who makes the decision.
注:维护人员必须使用指定任务的专用消耗材料。此类消耗材料已确认符合所有设计及认证要求。仅经批准的材料工程人员可决定使用等效消耗材料,相关组织须自行承担使用风险。
NOTE: You can get the full address and other information for vendors or suppliers listed in this table from the World Wide Web (www) at URL http://www.bpn.gov/bincs/begin_search.asp. Other CAGE Code sites are also available on the Web.
注:本表所列供应商的完整地址及其他信息可通过万维网(www)访问网址 http://www.bpn.gov/bincs/begin_search.asp 获取。其他CAGE代码网站亦可在网络上查阅。
暂无评论内容